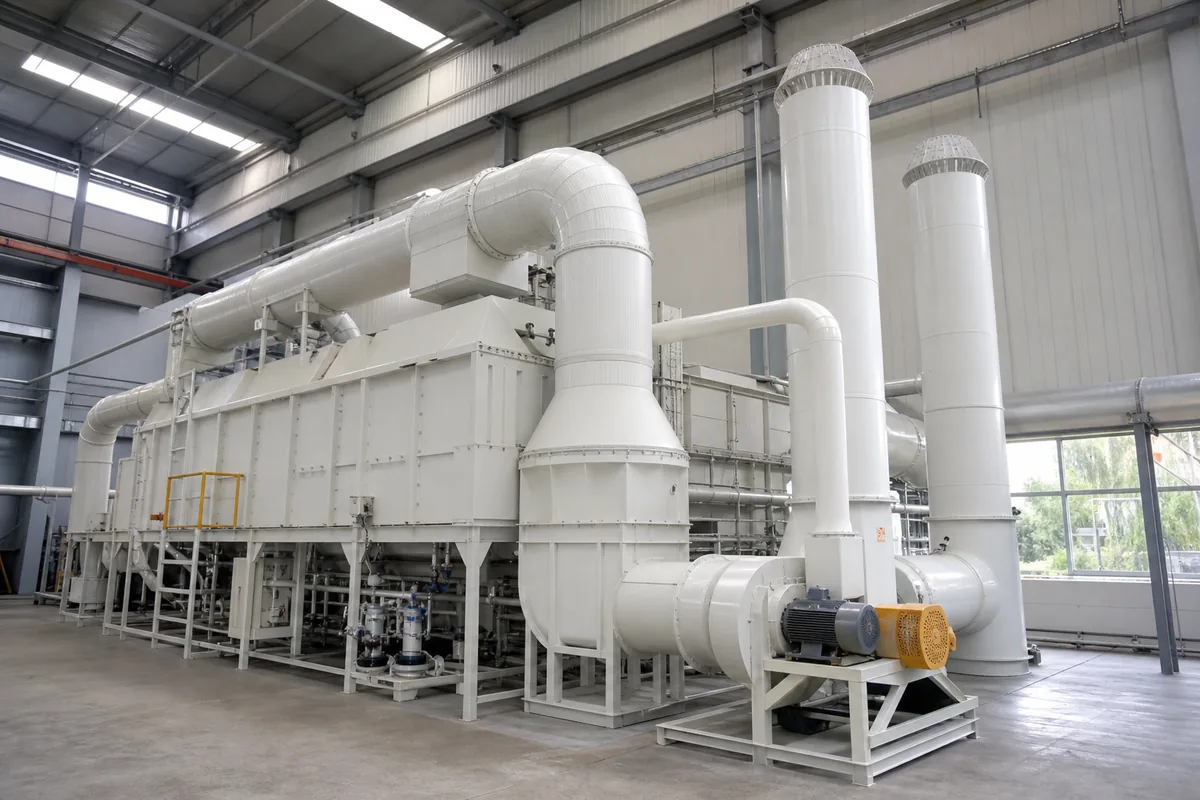
Why Low-Cost VOC Units Look Attractive
UV photolysis and low-temperature plasma VOC units are often sold as compact, low-pressure-drop alternatives to activated carbon, wet scrubbing, thermal oxidation, or catalytic oxidation. For small exhaust streams, they can look simple: install a box in the duct, connect power, and let lamps or plasma modules “break down” the VOCs.
In real factory exhaust systems, the result is more complicated. The main uv photolysis voc limitations are not only about UV lamp power. They also include gas composition, residence time, humidity, dust, oil mist, by-products, maintenance, and whether the VOC molecules can actually be destroyed at the installed energy density.
For plant engineers comparing options, the key question is not “Does UV or plasma work?” The better question is:
“For this exhaust gas, at this concentration, flow rate, humidity, and emission target, what removal efficiency can be achieved reliably without creating new problems?”
This article gives a practical comparison based on process engineering experience with VOC abatement systems, ducting, fans, scrubbers, activated carbon adsorbers, and combined treatment lines.
How UV Photolysis and Plasma Treat VOCs
UV photolysis units normally use UV lamps, often including 185 nm and/or 254 nm wavelengths. The treatment effect can come from several mechanisms:
- Direct photolysis of some VOC molecules
- Ozone generation from oxygen at 185 nm
- Oxidation by ozone and radicals
- Some sterilization effect, which is usually not the main goal for industrial VOC
Plasma units generate energetic electrons and reactive species by electrical discharge. These reactive species can attack VOC molecules. Common names include low-temperature plasma, non-thermal plasma, dielectric barrier discharge, and corona discharge.
In both technologies, the exhaust gas passes through a reaction zone. The available treatment time is short. A simple estimate is:
`text Residence time (s) = reactor effective volume (m³) / gas flow rate (m³/s) `
For many compact duct-mounted units, residence time is often only 0.1–1.0 seconds. This is much shorter than the seconds to minutes available in packed wet scrubbers, carbon beds, or thermal oxidizers. Therefore, performance depends heavily on VOC type and energy input.
A useful engineering indicator is specific energy input:
`text Specific energy input (Wh/m³) = electrical power to lamps or plasma (W) / gas flow rate (m³/h) `
For low-cost units, installed values may be only 1–10 Wh/m³. Some difficult VOCs require much higher energy to destroy meaningfully. If a supplier gives high removal efficiency but the energy input is very low, the data should be checked carefully.
Practical Comparison: UV, Plasma, Carbon, and Oxidation
The table below compares common VOC control technologies for typical industrial exhaust. Actual selection depends on VOC species, concentration, airflow, temperature, humidity, dust, and emission limit.
| Technology | Typical suitable range | Strengths | Main limits | Common engineering notes |
|---|---|---|---|---|
| UV photolysis | Low VOC concentration, relatively clean gas, odor polishing | Compact, low pressure drop, simple installation | Limited destruction for many VOCs; lamp fouling; ozone by-products | Better as pre-treatment or polishing, not as main control for high-load VOC |
| Low-temperature plasma | Low to moderate concentration, odor reduction, clean gas | Compact, fast reaction, can reduce some odors | By-products, ozone/NOx risk, unstable with humidity/oil/dust | Needs good pre-filtration and realistic performance testing |
| Activated carbon adsorption | Low to moderate concentration; intermittent or variable VOC load | High removal for many organic vapors; simple operation | Carbon replacement/regeneration; fire risk for high concentration or ketones | Check breakthrough time and bed temperature; use pre-filter for mist/dust |
| Wet scrubber | Water-soluble or chemically reactive gases | Good for acid/alkali gases; handles dust/mist | Poor for hydrophobic VOCs unless chemical absorption is suitable | Often used before carbon/UV/plasma to remove acid mist or particles |
| Catalytic/thermal oxidation | Medium to high VOC load, continuous operation | High destruction efficiency when designed correctly | Higher capital/energy demand; needs temperature control | Often best for strict emission limits and stable VOC streams |
UV and plasma may be useful, but they should not be treated as universal VOC destroyers. For many exhaust gases, activated carbon or oxidation gives more predictable performance.
Main Limitations Engineers Should Check
1. VOC molecule type matters
Simple odor compounds can sometimes be reduced enough for site comfort. But many industrial solvents are harder to destroy completely at short residence time.
Typical solvent groups that need careful evaluation include:
- Aromatics: toluene, xylene, styrene
- Ketones: acetone, MEK, MIBK
- Esters: ethyl acetate, butyl acetate
- Alcohols: IPA, ethanol, methanol
- Chlorinated VOCs: dichloromethane, trichloroethylene
- Mixed paint or printing solvent exhaust
Some molecules may be partially oxidized into aldehydes, organic acids, or other intermediates. A lower odor does not always mean full mineralization to CO₂ and H₂O.
2. Concentration range is limited
Low-cost UV or plasma units are usually more suitable for low VOC concentration, often below a few hundred mg/m³. When VOC concentration rises, required energy increases. If the unit is undersized, removal efficiency drops quickly.
As a rough rule:
- <50 mg/m³: UV/plasma may help with odor polishing if gas is clean.
- 50–300 mg/m³: possible, but must test with real gas and target compounds.
- 300–1,000 mg/m³: be cautious; carbon adsorption, condensation, or oxidation may be more realistic.
- >1,000 mg/m³: UV/plasma alone is rarely the first choice for reliable compliance.
These are not fixed limits. A highly reactive odor compound at low flow is different from a mixed solvent stream at high flow.
3. Dust, oil mist, and humidity reduce performance
UV lamps need a clean optical surface. If dust, tar, resin, paint mist, or oil coats the lamp sleeve, UV intensity drops. A lamp that still lights visually may have much lower useful output.
Plasma modules can also foul. Sticky deposits may cause discharge instability, arcing, higher pressure drop, and fire risk if combustible deposits build up.
For many real systems, pre-treatment is not optional:
- Grease/oil mist filter before UV/plasma
- Bag or cartridge filter for dust
- Wet scrubber or demister for acid mist
- Cooling or dilution if temperature is high
- Drain and access doors for maintenance cleaning
Relative humidity above 70–80% can reduce effective oxidation chemistry in some designs and increase corrosion or condensation problems. If the gas is near dew point, condensate may collect in the unit and duct.
4. By-products may be more important than inlet VOC
UV at 185 nm can generate ozone. Plasma can also generate ozone and, in air, may form NOx. Partial oxidation can create aldehydes such as formaldehyde or acetaldehyde, depending on the VOC.
Therefore, performance should not be judged only by odor or total hydrocarbon reduction. For serious applications, check:
`text Inlet VOC species + outlet VOC species + ozone + aldehydes + CO + NOx `
If the outlet is discharged indoors or near workers, ozone is especially important. Even if local regulations allow outdoor discharge, high ozone release can create safety and odor complaints.
A common design approach is to place activated carbon after UV/plasma to capture residual VOC and ozone by-products. However, ozone can heat and oxidize carbon, so the design must consider temperature, residence time, and fire protection.
5. Lamp and module aging changes performance
UV lamp output decreases with operating time. A lamp may still be on after 8,000 hours, but UV intensity can be much lower than new. For many low-pressure mercury lamps, useful life is often around 6,000–9,000 hours, depending on lamp quality, temperature, and switching frequency.
Plasma modules also age due to electrode fouling, dielectric damage, corrosion, and dust accumulation. Maintenance intervals vary widely, but inspection every 1–3 months is common in dirty exhaust service.
For procurement, ask not only for equipment dimensions, but also:
- Lamp wavelength and power
- Number of lamps and total installed electrical power
- Recommended replacement interval
- Access space needed for lamp removal
- Cleaning method for lamp sleeves or modules
- Pressure drop when clean and when dirty
- Interlock for access doors and high voltage
- Ozone control method
When UV or Plasma Can Be Reasonable
UV photolysis and plasma are not useless. They can be reasonable when the application is selected correctly.
They may fit:
- Low-concentration odor control where the target is odor reduction, not high VOC destruction
- Exhaust after good mist and dust removal
- Polishing stage after a wet scrubber, carbon bed, or biological system
- Small airflow systems where carbon replacement logistics are difficult
- Intermittent sources with low solvent load
- Applications where site testing proves the result
They are usually weak choices when:
- VOC concentration is high or strongly variable
- Solvent recovery value is important
- Emission limit is strict and legally measured
- Gas contains heavy oil mist, paint overspray, resin, tar, or sticky aerosol
- Gas contains chlorinated or sulfur-containing VOCs that may form corrosive by-products
- Maintenance access is poor
- The buyer expects “install and forget” operation
For comparison, activated carbon adsorption is often more predictable for many solvent vapors at low to medium concentration. A simple carbon sizing check starts with the VOC mass load:
`text VOC mass load (kg/h) = airflow (m³/h) × VOC concentration (mg/m³) / 1,000,000 `
If airflow is 10,000 m³/h and VOC concentration is 100 mg/m³:
`text 10,000 × 100 / 1,000,000 = 1.0 kg/h VOC `
If carbon working capacity is estimated at 5–15% by weight depending on VOC and humidity, then 1,000 kg of carbon may hold roughly 50–150 kg before breakthrough. This is only a rough calculation, but it gives a more concrete maintenance estimate than many UV/plasma proposals.
For oxidation systems, the design focus is different: temperature, residence time, turbulence, heat recovery, catalyst selection if catalytic, and safety controls. Energy use may be higher, but destruction efficiency can be much more dependable when the system is correctly engineered.
A Practical Next Step
Before selecting a low-cost UV or plasma VOC unit, prepare a one-page gas data sheet:
- Airflow: normal, minimum, maximum in m³/h
- VOC names and concentrations in mg/m³
- Temperature and relative humidity
- Dust, oil mist, acid mist, or water droplets present
- Operating hours per day
- Required outlet limit and test method if known
- Available installation space and maintenance access
Then ask suppliers to calculate residence time, specific energy input, expected by-products, pressure drop, and maintenance interval. If possible, test with real exhaust gas. UV and plasma can be useful tools, but only when their limits are designed into the system instead of ignored.