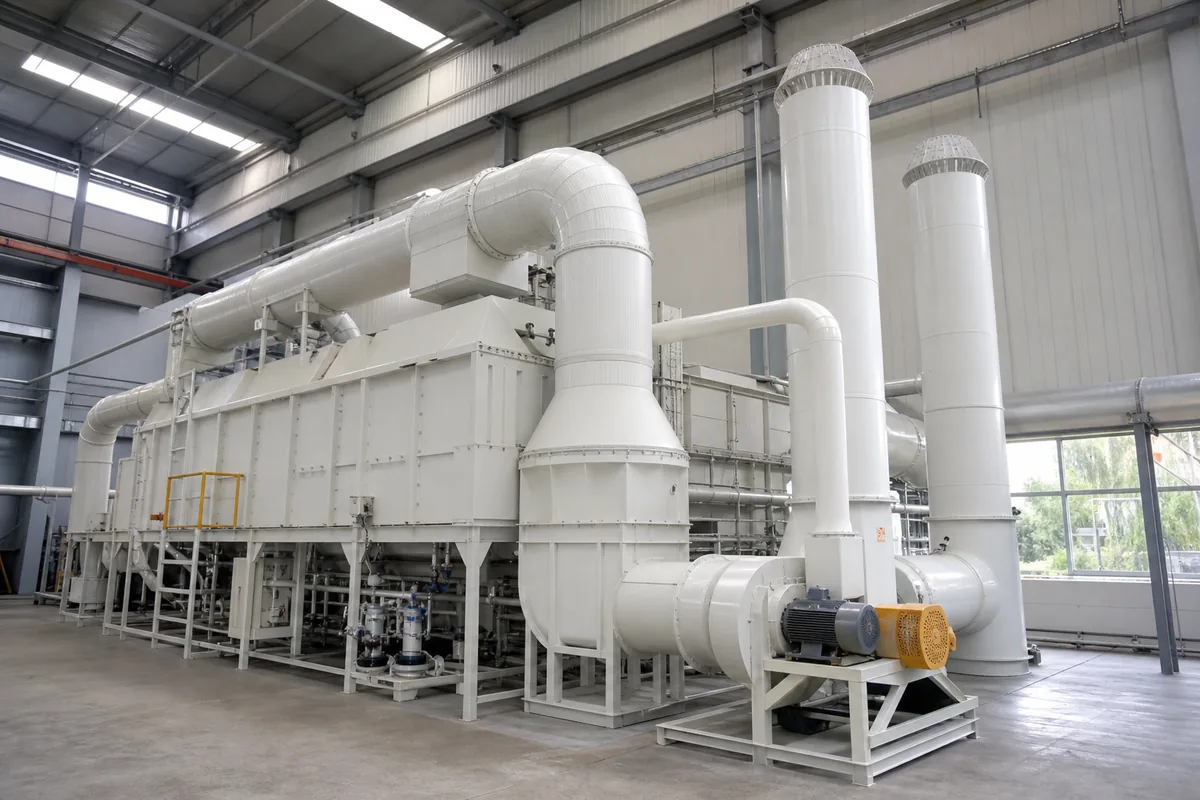
Why Heat Recovery Matters in VOC Abatement
Many VOC abatement systems use heat to destroy or desorb organic compounds. This includes regenerative thermal oxidizers (RTO), recuperative thermal oxidizers, catalytic oxidizers, and some activated carbon desorption systems. In these systems, the energy cost is often not the fan power. It is the fuel or electric heat required to raise the exhaust gas to the required treatment temperature.
This is where voc system heat recovery creates payback. The basic idea is simple: use the hot clean exhaust leaving the treatment unit to preheat the incoming dirty gas, or recover heat for another plant process.
For a thermal oxidizer, a simple heat balance is:
`text Heat required = Gas flow × Gas heat capacity × Temperature rise `
For air at normal conditions, a practical rule is:
`text Heat load (kW) ≈ Airflow (Nm³/h) × ΔT (°C) × 0.00033 `
Example:
- Airflow: 10,000 Nm³/h
- Inlet temperature: 30°C
- Oxidation temperature: 800°C
- Temperature rise without heat recovery: 770°C
`text Heat load ≈ 10,000 × 770 × 0.00033 = 2,541 kW `
In real operation, some heat is supplied by the VOC itself. But for low VOC concentration exhaust, the auxiliary fuel can still be high. Heat recovery reduces this load.
Main Sources of Payback
The payback from heat recovery normally comes from four areas.
1. Lower auxiliary fuel or electric heating
This is the largest saving in most thermal VOC systems. If a heat exchanger recovers 60% of the heat from the hot outlet gas, the burner does not need to supply that part of the temperature rise.
Using the earlier example:
`text Recovered temperature rise = 770°C × 60% = 462°C Remaining temperature rise = 308°C Remaining heat load ≈ 10,000 × 308 × 0.00033 = 1,016 kW `
The theoretical saving is about:
`text 2,541 - 1,016 = 1,525 kW `
Actual saving will be lower after considering heat exchanger loss, burner efficiency, pressure drop, bypass leakage, VOC heat release, and operating load changes. Still, this calculation shows why heat recovery is important.
2. Higher chance of autothermal operation
A VOC oxidizer is called autothermal when the VOC heat content is enough to maintain operating temperature without auxiliary fuel, except during start-up or low-load periods.
As a rough engineering guide:
- Low heat recovery oxidizer may need higher VOC concentration to be autothermal.
- High heat recovery RTO may become autothermal at much lower VOC concentration.
- The exact point depends on VOC type, LEL safety dilution, airflow, oxidation temperature, and heat losses.
For many solvent vapors, a rough heating value range is 20–40 MJ/kg VOC. If the VOC concentration is 1 g/Nm³ and the heating value is 30 MJ/kg:
`text VOC heat input = 1 g/Nm³ × 10,000 Nm³/h × 30 MJ/kg = 300 MJ/h ≈ 83 kW `
This is small compared with a 1,000–2,000 kW heating load. Therefore, dilute exhaust usually needs strong heat recovery or concentration before oxidation.
3. Reuse of recovered heat in production
Sometimes the best payback is not only inside the oxidizer. The clean hot gas can be used to heat:
- Oven make-up air
- Drying air
- Process water
- Cleaning tanks
- Boiler feedwater preheating
- Workshop heating in cold climates
The practical limit is temperature matching. High-temperature heat should be used for high-temperature demand. Low-temperature heat should be used for water or space heating. If the recovered air is 120°C, it cannot directly supply a 180°C oven without extra heating.
A common design approach is to list plant heat users by required temperature and operating time. Heat recovery has better payback when the heat source and heat user operate at the same time.
4. Smaller utility infrastructure
Reducing burner duty can also reduce the load on gas supply piping, electrical heaters, transformers, and ventilation for combustion air. This may not always be the main saving, but it can affect plant layout and permitting discussions. The benefit depends strongly on local utilities and site conditions.
Common Heat Recovery Methods
Different VOC systems use different heat recovery equipment. The correct choice depends on temperature, dust loading, corrosion risk, VOC composition, safety requirements, and maintenance access.
| Heat recovery method | Typical use | Typical heat recovery range | Advantages | Main concerns |
|---|---|---|---|---|
| Regenerative ceramic bed | RTO | 85–95% thermal efficiency | Very high recovery, suitable for large airflow | Larger footprint, valve maintenance, not ideal for sticky particulate |
| Metallic recuperative heat exchanger | Recuperative oxidizer, catalytic oxidizer | 40–75% | Simple continuous flow, easier control | Thermal stress, fouling, corrosion at dew point |
| Plate or tube air-to-air exchanger | Low to medium temperature exhaust | 30–70% | Good for clean air streams | Leakage risk, pressure drop, cleaning access |
| Air-to-water heat exchanger | Recover heat for hot water | Depends on water temperature and flow | Useful when plant needs hot water | Condensation, corrosion, water-side scaling |
| Rotary heat exchanger | Some low-temperature VOC ventilation systems | 50–80% | Compact | Possible cross-contamination, seal leakage, VOC safety review needed |
For high-temperature VOC destruction, regenerative ceramic systems usually give the highest internal heat recovery. For lower-temperature exhaust, external heat exchangers may be easier to justify.
How to Estimate Payback Step by Step
A reliable payback estimate should use plant operating data, not only nameplate values. The following method is practical for early engineering.
Step 1: Define the exhaust condition
Collect these values:
- Normal and maximum airflow, Nm³/h
- Exhaust temperature, °C
- VOC concentration, mg/Nm³ or ppmv
- VOC composition or representative solvent
- Moisture content
- Dust, mist, resin, tar, or acid gas content
- Operating hours per year
- Required treatment temperature and residence time, if known
Use normal airflow for energy calculation and maximum airflow for equipment sizing.
Step 2: Calculate gross heat demand
Use:
`text Q = Flow × ΔT × 0.00033 `
Where:
Q= heat load, kWFlow= Nm³/hΔT= temperature rise, °C
For catalytic oxidizers, operating temperature may be 250–450°C depending on catalyst and VOC type. For thermal oxidizers, it is often 750–850°C, but this depends on destruction requirement and gas composition.
Step 3: Estimate recovered heat
`text Recovered heat = Gross heat demand × Heat recovery efficiency `
Example:
- Flow: 20,000 Nm³/h
- Inlet: 40°C
- Treatment: 800°C
- ΔT: 760°C
- Gross heat load:
20,000 × 760 × 0.00033 = 5,016 kW - Heat recovery: 90%
`text Remaining theoretical heat = 5,016 × (1 - 0.90) = 502 kW `
This is before considering VOC heat release and losses. If the VOC contributes 150 kW, the net auxiliary heat may be about 350 kW plus system losses.
Step 4: Convert energy saving to annual saving
`text Annual energy saving = Average saved kW × Operating hours per year `
Then convert to gas, steam, or electricity using the local energy unit and heater efficiency. Do not forget part-load operation. A system running 8,000 hours per year has very different payback from one running 1,500 hours per year.
Step 5: Subtract extra operating costs
Heat recovery is not free. Include:
- Higher fan power from added pressure drop
- Cleaning labor and downtime
- Replacement of seals, valves, gaskets, or packing
- Condensate treatment if water or acid condenses
- Instrumentation and control maintenance
- Possible production loss during exchanger cleaning
A typical clean air-to-air exchanger may add 300–1,000 Pa pressure drop. RTO ceramic beds and valves can add more, depending on design and fouling. Fan power can be estimated by:
`text Fan power (kW) = Flow (m³/s) × Pressure (Pa) / Fan efficiency / 1000 `
If 20,000 m³/h equals 5.56 m³/s, added pressure drop is 800 Pa, and fan efficiency is 60%:
`text Extra fan power = 5.56 × 800 / 0.60 / 1000 = 7.4 kW `
This is usually much smaller than thermal saving, but it should be counted.
Design Risks That Can Reduce Payback
The payback calculation can look good on paper but fail in operation if the gas stream is not suitable. Check these points early.
Fouling
Paint mist, resin, oil mist, adhesive vapor, plasticizer, or dust can block heat transfer surfaces or ceramic beds. Fouling reduces heat recovery and increases pressure drop. For dirty gas, consider:
- Better pre-filtration or demister
- Washable pre-scrubber
- Access doors for cleaning
- Lower face velocity
- Bypass for maintenance
Corrosion and condensation
If the exhaust contains acid gases, chlorine compounds, sulfur compounds, or high moisture, condensation can create corrosive liquid. Metal heat exchangers are vulnerable near acid dew point. PP equipment is useful for low-temperature corrosive gas handling, but PP cannot be used at thermal oxidizer temperatures. Material selection must match the local gas temperature.
Safety and LEL control
Heat recovery raises inlet temperature. This can affect lower explosive limit margin. Many VOC systems are designed to keep VOC concentration below a defined fraction of LEL by dilution and monitoring. The exact safety philosophy must be reviewed by qualified safety engineers.
Heat user mismatch
External heat recovery needs a stable heat user. If the oven or water tank only operates part of the time, recovered heat may be vented. Payback becomes longer. A heat storage tank can help for hot water, but it adds complexity.
Practical Next Step
Before selecting equipment, prepare a one-page heat recovery data sheet: airflow, temperature, VOC type and concentration, moisture, contaminants, operating hours, and possible heat users. With these values, an engineer can calculate the gross heat load, estimate realistic recovery, check fouling and corrosion risks, and decide whether voc system heat recovery should be internal, external, or not applied for that gas stream.


