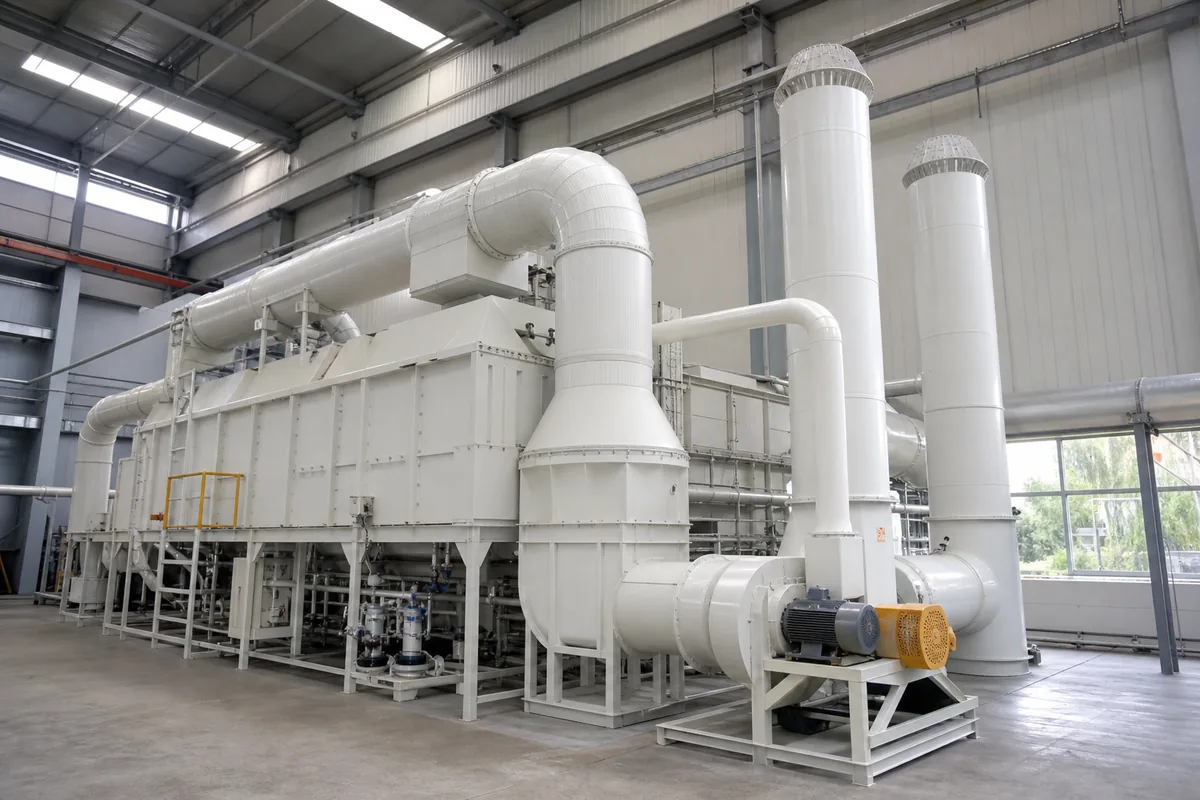
Why Catalyst Poisoning Matters in VOC Oxidizers
A catalytic VOC oxidizer destroys volatile organic compounds at lower temperature than a thermal oxidizer. Typical catalyst inlet temperatures are 250–400°C, depending on VOC type, concentration, catalyst formulation and required destruction efficiency. This saves fuel, but the catalyst surface must remain active.
Catalyst poisoning in a VOC oxidizer means that contaminants in the exhaust gas react with, coat or block the active catalytic sites. The result is usually seen as:
- Higher temperature needed to achieve the same VOC removal
- Lower destruction efficiency at the original setpoint
- Increased pressure drop if deposits form
- Hot spots or uneven bed temperature
- Short catalyst life and more frequent replacement
Three common poison groups are silicon, sulfur and halogens. They behave differently, so the correct engineering response is also different. In many plants, poisoning is not caused by one large event, but by low-level contamination over months.
A simple check is to trend the catalyst bed performance:
`text Temperature rise across catalyst bed ≈ heat released by VOC oxidation `
If VOC loading is stable but outlet VOC increases, or if the same removal requires a higher inlet temperature, the catalyst may be losing activity. Before assuming the catalyst is bad, also check flow, bypass leakage, burner control, thermocouple position and sample point location.
Silicon: Small Concentrations Can Create Permanent Coating
Silicon compounds are one of the most serious poisons for many oxidation catalysts. In VOC systems they often come from:
- Silicone oils, mold release agents and lubricants
- Siloxanes in personal care, coating or printing processes
- Sealants, anti-foam agents and defoamers
- Some adhesives and rubber processing fumes
- Landfill gas or biogas, if used as auxiliary fuel
During oxidation, organic silicon compounds can form silica-like deposits on the catalyst surface. This is similar to putting a thin glass layer over the active sites. Once formed, this layer is usually difficult or impossible to remove by normal burn-off.
Typical risk levels depend strongly on the catalyst and gas composition, but as a conservative rule:
- Continuous silicon-containing VOC should be treated as high risk
- Even single-digit ppmv levels of siloxanes may shorten catalyst life
- Intermittent high peaks can be worse than a low average value
Silicon poisoning often shows a gradual activity loss. The catalyst bed may look visually clean, because the deposit can be very thin. Pressure drop may remain normal. This makes laboratory gas analysis and inlet material review important.
Practical engineering actions:
- Identify silicon sources before selecting catalytic oxidation. Ask production for all additives, release agents, lubricants and defoamers used near the exhaust source.
- Consider upstream removal. Activated carbon or special adsorbents may capture some silicon compounds, but capacity varies. Test data is important.
- Use a sacrificial guard bed where suitable. A lower-cost pre-bed can take part of the contamination before the main catalyst.
- Avoid silicone sealants in hot gas paths. For duct flanges and inspection doors, choose gasket materials suitable for the temperature and gas chemistry.
For processes with unavoidable siloxanes, a thermal oxidizer may be more robust, although fuel use is higher. The choice depends on VOC concentration, operating hours and contaminant level.
Sulfur: Reversible or Permanent Depending on Chemistry
Sulfur compounds are common in chemical, rubber, resin, food, wastewater and fuel-related exhausts. Examples include:
- Hydrogen sulfide, H₂S
- Mercaptans and thiols
- Carbon disulfide, CS₂
- Sulfur dioxide, SO₂
- Sulfur-containing solvents or additives
In a catalytic VOC oxidizer, sulfur can occupy active sites and reduce oxidation activity. Some sulfur poisoning is partly reversible at higher temperature or with clean gas operation. However, sulfur can also form stable sulfates on the catalyst or support, especially with certain metals and operating conditions.
A key point is that sulfur oxidation forms SO₂ and sometimes SO₃. If moisture is present and the gas cools below the acid dew point, sulfuric acid corrosion can occur downstream.
Approximate engineering reference values:
| Item | Typical Range or Rule of Thumb | Engineering Note |
|---|---|---|
| SO₂ acid dew point risk | Often 120–180°C, depending on SO₃ and moisture | Keep downstream surfaces above dew point or use corrosion-resistant materials |
| Catalyst inlet temperature | Often 250–400°C | Higher temperature may reduce temporary sulfur inhibition, but may not solve permanent sulfate formation |
| Sulfur screening level | Any continuous sulfur compound should be reviewed | Acceptable level depends on catalyst formulation and required life |
| Downstream material | PP, FRP or lined steel may be used in cool wet sections | Temperature limit and chemical resistance must match actual conditions |
For sulfur-containing exhaust, do not look only at VOC destruction. Also evaluate the final acid gas load. In some systems, a wet scrubber after the oxidizer is used to remove SO₂ or acid mist. If the gas temperature entering a PP scrubber is too high, a quench section is needed. PP equipment is commonly used at lower temperatures, but design temperature must be checked carefully for each project.
Important design questions include:
- What sulfur compounds are present, and at what maximum concentration?
- Is the sulfur continuous or only during cleaning, startup or product change?
- Will the oxidizer convert reduced sulfur to SO₂ efficiently?
- Is an acid gas scrubber required after oxidation?
- What materials are suitable for ducting, fan casing and stack after cooling?
Halogens: Catalyst Risk Plus Acid Gas and Corrosion
Halogens include chlorine, fluorine, bromine and iodine compounds. In VOC exhaust, the most common concern is chlorinated solvent or fluorinated organic compounds. Examples include methylene chloride, trichloroethylene, perchloroethylene, chlorobenzene and some fluorinated process gases.
Halogenated VOCs create two problems:
- They can poison or deactivate some catalysts.
- Oxidation produces acid gases such as HCl and HF.
HF is especially aggressive and requires careful material selection. HCl is also corrosive, especially when moisture is present.
A simplified stoichiometric example:
`text CH2Cl2 + O2 → CO2 + 2 HCl `
This means one mole of methylene chloride can form two moles of HCl. For preliminary estimation:
`text Acid gas molar flow = VOC molar flow × number of halogen atoms per molecule `
For concentration conversion at normal conditions, a useful approximation is:
`text mg/Nm³ = ppmv × molecular weight / 22.4 `
At 25°C, some engineers use 24.45 instead of 22.4. Use one basis consistently.
Halogenated exhaust often needs a system arrangement such as:
- Oxidizer for VOC destruction
- Quench to reduce gas temperature
- Packed wet scrubber with alkaline recirculation
- Mist eliminator
- Corrosion-resistant fan and ducting
For alkaline HCl scrubbing, caustic soda is commonly used. The theoretical reaction is:
`text HCl + NaOH → NaCl + H2O `
In practice, use a control margin because of mass transfer efficiency, pH control delay and concentration peaks. Many packed scrubbers operate with recirculation liquid pH around 8–10 for acid gas service, but the correct setpoint depends on emission target, scaling risk and wastewater requirements.
Catalytic oxidizers can treat some halogenated VOC streams if the catalyst is selected for that service and acid gas handling is included. However, high halogen loading can make a thermal oxidizer with downstream scrubbing more practical. This is an application-specific decision.
How to Diagnose and Reduce Poisoning Risk
When a plant reports reduced oxidizer performance, the first step is to separate catalyst poisoning from mechanical or control problems. Use a structured check:
- Measure inlet and outlet VOC under stable production conditions.
- Record catalyst inlet, middle and outlet temperatures.
- Check total airflow; higher flow reduces residence time.
- Inspect for bypass leakage around dampers, gaskets and catalyst modules.
- Measure pressure drop across filters, heat exchanger and catalyst bed.
- Review recent production changes, including new raw materials and cleaning agents.
- Analyze for Si, S, Cl, F, Br compounds if poisoning is suspected.
For a fixed-bed catalyst, space velocity is a key design and troubleshooting parameter:
`text GHSV = gas flow rate at operating condition / catalyst volume `
Common catalytic oxidizer GHSV values may be in the range of 10,000–40,000 h⁻¹, depending on catalyst type, VOC reactivity and required performance. Higher GHSV means shorter contact time. If the system was designed near the limit, small activity loss becomes visible quickly.
Risk reduction measures are best applied before the oxidizer:
| Contaminant Group | Typical Source | Main Risk | Possible Control |
|---|---|---|---|
| Silicon | Siloxanes, silicone oil, release agents | Permanent surface coating | Source substitution, upstream adsorbent, guard bed |
| Sulfur | H₂S, mercaptans, CS₂, sulfur additives | Activity loss, SO₂/SO₃, acid corrosion | Source control, catalyst selection, downstream scrubber |
| Halogens | Chlorinated or fluorinated solvents | Catalyst deactivation, HCl/HF formation | Process segregation, thermal oxidation review, quench and alkaline scrubber |
Good operation also helps. Avoid long operation at low catalyst temperature with heavy VOC loading, because incomplete oxidation can create deposits. Avoid sudden high-concentration slugs. If batch emissions are unstable, consider a buffer tank, concentration equalization, or activated carbon adsorption followed by controlled desorption.
Practical Next Step
If your VOC oxidizer is losing performance, prepare a simple data package before changing equipment:
- VOC list with maximum and normal concentrations
- Gas flow range, temperature and humidity
- Known silicon, sulfur and halogen sources
- Current oxidizer temperature trend and pressure drop
- Inlet and outlet VOC test results under the same production condition
With this information, an equipment supplier or catalyst specialist can judge whether the issue is likely catalyst poisoning in the VOC oxidizer, poor operating conditions, or a need for pretreatment such as activated carbon adsorption, wet scrubbing, quench cooling or process segregation.