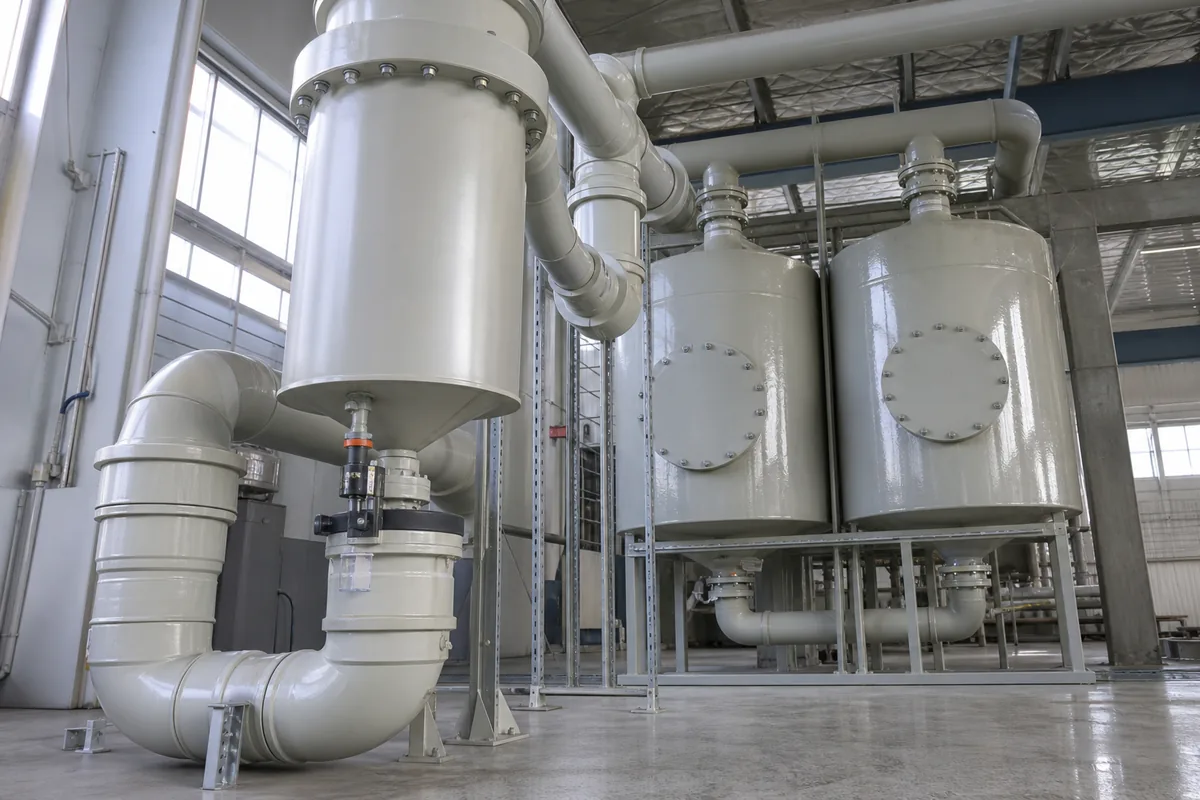
The Failure Mode: Carbon Looks Full, but VOC Is Still Passing
Activated carbon adsorbers are simple and reliable when the gas is dry enough. When the exhaust is humid, the same carbon bed can fail much earlier than expected. This is one of the most common problems we see in VOC treatment systems installed after washing tanks, wet scrubbers, plating lines, printing lines, food processing, and wastewater ventilation.
The humidity effect activated carbon users often notice is:
- VOC odor appears at the stack after only a short running time.
- Carbon replacement frequency becomes much higher than the design estimate.
- Pressure drop rises because the bed becomes wet or contaminated.
- Carbon at the inlet side feels damp, sticky, or caked.
- The fan current increases due to higher system resistance.
- In severe cases, liquid water drains from the carbon vessel.
The root cause is usually not “bad carbon.” It is water vapor, mist, or condensation entering the bed.
Activated carbon works by adsorbing molecules on internal pore surfaces. A good vapor-phase carbon may have a surface area of 800–1,200 m²/g. VOC molecules need access to these pores. Water also adsorbs into the same pore structure, especially at high relative humidity. Once water occupies the small pores, VOC capacity drops quickly.
A common rule of thumb:
- Below 50% RH: carbon performance is usually stable for many VOCs.
- 50–70% RH: capacity starts to reduce, depending on VOC type.
- Above 70% RH: capacity loss can be significant.
- Above 85–90% RH: risk of early breakthrough, condensation, and bed wetting is high.
- Any visible mist or liquid droplets: not acceptable for normal activated carbon beds.
These values are not universal. Ketones, alcohols, and other polar compounds are more affected by water than many hydrocarbons and solvents such as toluene or xylene. Temperature, inlet concentration, carbon type, and contact time also matter.
Why Humidity Damages Adsorption Capacity
There are three different water problems. They are often mixed together, but they should be solved differently.
1. High relative humidity
Relative humidity is the percentage of water vapor in the gas compared with the maximum amount the gas can hold at that temperature. Warm gas can carry more water vapor than cold gas.
For carbon adsorption, relative humidity is more important than “the gas feels dry.” A 40°C exhaust can contain a large amount of water, but if it is reheated above its dew point, the RH may still be moderate.
The approximate relationship is:
`text RH (%) = actual water vapor pressure / saturation vapor pressure at gas temperature × 100 `
When RH rises, water adsorption increases. This reduces the effective VOC working capacity. For many solvent VOCs, a dry carbon working capacity may be 8–20% of carbon weight. At high humidity, it may fall to 3–8%, or even lower for polar VOCs.
2. Mist carryover
Mist means small liquid droplets in the gas stream. This is common after a wet scrubber, spray tower, quench, or open washing tank. Activated carbon is not designed as a mist eliminator.
Droplets can:
- Block the bed inlet surface.
- Carry salts, acid, alkali, oil, or surfactants into the carbon.
- Cause carbon dust to form sludge.
- Increase pressure drop.
- Create corrosion or leakage problems in downstream metal parts.
A carbon adsorber after a wet scrubber should always have a proper demister and drainage section before the carbon vessel.
3. Condensation inside the bed
Condensation is often the most serious problem. It happens when the exhaust temperature drops below its dew point inside ducting or inside the carbon bed.
Example:
- Exhaust leaves a scrubber at 35°C and near 100% RH.
- The duct passes through a cooler area.
- Gas temperature drops to 30°C.
- Water condenses in the duct and then enters the carbon bed.
Even if the inlet has no visible water, condensation can form later if the vessel wall is cold. This is common in outdoor installations, winter operation, long PP duct runs, and night shutdown/startup cycles.
Practical Limits Before a Carbon Bed
For most industrial VOC activated carbon adsorbers, we use the following design targets. Final values should be checked against the VOC mix, emission target, carbon selection, and site conditions.
| Parameter before carbon bed | Preferred range | Warning range | Why it matters |
|---|---|---|---|
| Relative humidity | <60% RH | 60–75% RH | Higher RH reduces VOC working capacity |
| Mist droplets | None visible | Any visible mist | Liquid water blocks pores and carries contaminants |
| Gas temperature above dew point | +5 to +10°C minimum | <+5°C | Prevents condensation in duct and vessel |
| Bed face velocity | 0.2–0.6 m/s | >0.8 m/s | High velocity reduces contact time and may entrain dust |
| Empty bed contact time | 0.5–2.0 s | <0.5 s | Short time causes early breakthrough |
| Carbon bed pressure drop | Often 800–1,500 Pa clean | Rising fast | Wet or dirty bed may be plugging |
The “cheap fix” is usually not a larger carbon bed. A bigger bed can still fail if wet gas enters it. The low-cost correction is normally remove droplets and control dew point margin before the carbon.
The Cheap Fix: Demist, Drain, and Reheat Slightly
For many systems, especially when carbon is installed after a wet scrubber, the most effective fix is a small preconditioning section:
- Install or improve a demister
- Add a drainable knock-out section
- Reheat the gas 5–10°C above its dew point
- Insulate cold ducting if needed
This is much cheaper and simpler than frequent carbon replacement, oversized vessels, or changing to more complex VOC technology.
Step 1: Use a real demister
A wet scrubber outlet should include a mist eliminator. Common options are PP chevron vane demisters or mesh pad demisters.
For corrosive exhaust, PP is often used because it resists many acids and alkalis. Typical design values:
- Vane demister gas velocity: 2–4 m/s, depending on droplet loading.
- Mesh pad gas velocity: often 1.5–3 m/s, depending on design.
- Pressure drop: commonly 100–400 Pa when clean.
- Add flushing nozzles if salts or solids are present.
- Provide a bottom drain with water seal or suitable trap.
A demister is not only a component. It needs enough straight space, correct orientation, and drainage. If the gas velocity is too high, droplets will re-entrain and pass downstream.
Step 2: Add a knock-out and drain point
After the demister, provide a low-point drain or small knock-out box before the carbon adsorber. This is important for long ducts and outdoor systems.
Good practice:
- Slope horizontal ducting slightly toward a drain point.
- Avoid low pockets where water can collect.
- Install an inspection window or removable cover if possible.
- Do not allow condensed liquid to enter the carbon vessel.
- Use chemical-resistant drain materials matched to the process gas.
For PP ducting, thermal expansion should also be considered. Long outdoor runs need proper supports and expansion allowance.
Step 3: Reheat above dew point
If gas leaves a scrubber saturated, demisting alone removes droplets but does not reduce relative humidity enough. The gas may still be at 95–100% RH. A small temperature increase can reduce RH and prevent condensation.
Example: air saturated at 35°C has 100% RH. If reheated to about 45°C without adding more water, RH drops to roughly 55–60%. This is often enough to protect the carbon bed.
Rule of thumb:
`text Target gas temperature = dew point + 5 to 10°C `
Heating methods depend on the plant:
- Electric duct heater for small airflows.
- Steam or hot water coil where utilities are available.
- Heat recovery from a hot exhaust stream.
- Mixing with a small amount of warmer dry air, if process rules allow.
Do not overheat unnecessarily. Higher temperature can reduce VOC adsorption capacity. Many carbon systems work best around 20–40°C. If the gas must be kept hotter to prevent condensation, carbon sizing should be checked carefully.
When the Simple Fix Is Not Enough
Demist and reheat solve many humidity-related failures, but not all. More engineering is needed in these cases:
- VOC concentration is very high and adsorption heat may create temperature rise.
- VOCs are water-soluble and the upstream scrubber removes part of them.
- Exhaust contains oil mist, resin, tar, silicone, or sticky aerosol.
- Gas contains acid/alkali mist that can attack carbon or create salts.
- Required outlet concentration is very low.
- Operation is intermittent, causing frequent cooling and condensation.
- Relative humidity must stay high because of process safety or product quality.
In these cases, other options may be considered: better pre-filtration, condenser, dehumidifier, hydrophobic carbon, impregnated carbon, zeolite rotor, catalytic oxidation, thermal oxidation, or a combined scrubber + adsorption system. The correct choice depends on airflow, VOC type, concentration, temperature, humidity, dust/mist loading, and discharge requirement.
Practical Next Step
Before replacing carbon again, measure the gas condition at the carbon inlet:
- Airflow: m³/h
- Temperature: °C
- Relative humidity: %
- Dew point: °C
- VOC type and concentration: mg/m³ or ppm
- Pressure drop across demister and carbon bed: Pa
- Any visible mist, drain water, or wet carbon condition
If RH is above 70%, if dew point margin is less than 5°C, or if any mist is present, fix the inlet condition first. In many plants, a correctly sized PP demister, drain section, and small reheat margin will extend carbon life much more effectively than simply installing more carbon.


