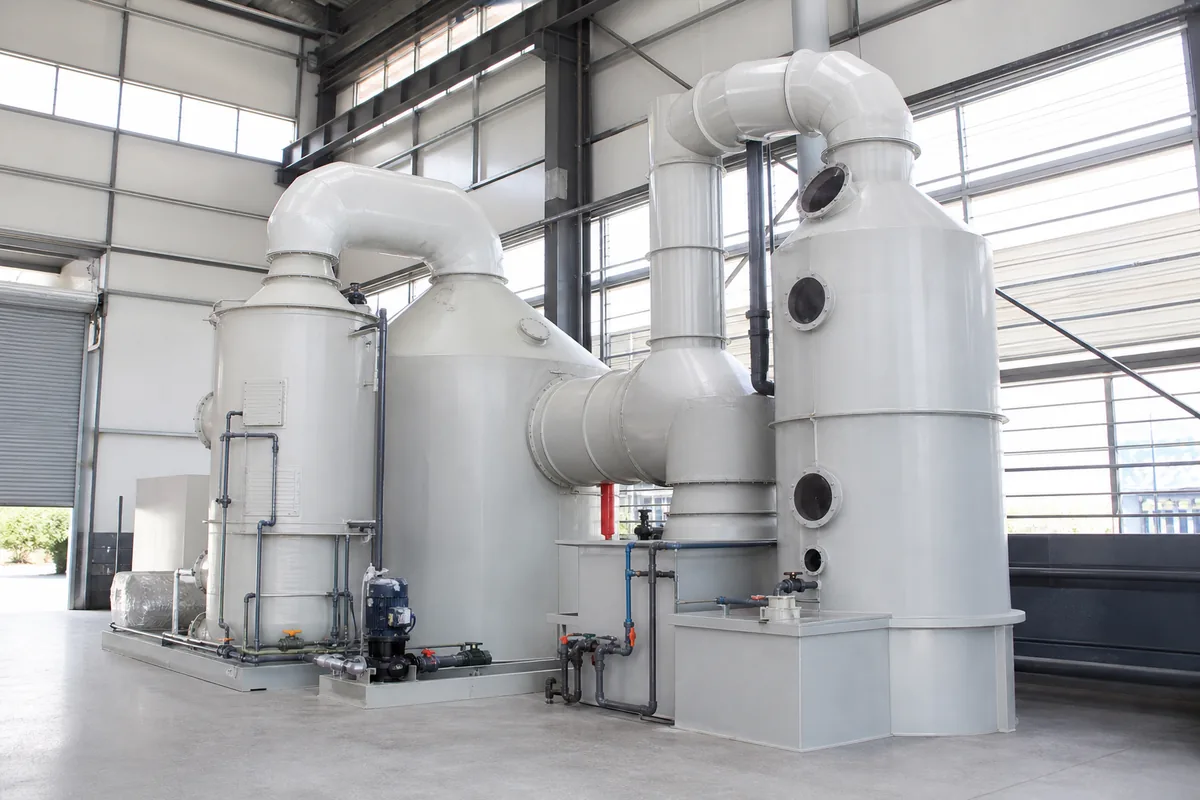
Why a Venturi Stage Is Added Before the Main Scrubber
In many exhaust systems, the first design question is not “Which scrubber removes the gas?” but “Will dust, mist, or sticky particles block the main scrubber?” This is where a venturi scrubber application becomes important.
A venturi scrubber is often used as a pre-scrubbing stage before a packed bed scrubber, tray scrubber, demister, activated carbon adsorber, or VOC treatment unit. Its main job is to remove particulate matter and aerosols before they reach more sensitive equipment.
Typical problem cases include:
- Acid mist mixed with fine solids
- Alkali dust from chemical handling
- Soluble powder carryover from reactors or dryers
- Sticky organic aerosol before activated carbon
- Fume containing both gas pollutants and particles
- High-temperature gas that needs quenching and cleaning
A packed tower is good for gas absorption, but it is not a dust collector. If heavy particulate enters the packing, the tower can suffer from plugging, high pressure drop, poor liquid distribution, and difficult maintenance. A venturi scrubber placed upstream can reduce this risk.
The comparison is simple:
- Packed tower: better for soluble gas removal, low to medium dust loading
- Venturi scrubber: better for particulate and mist removal, especially fine particles
- Combined system: used when both particulate and gas pollutants must be controlled
For many chemical, pharmaceutical, metal finishing, fertilizer, and waste gas treatment systems, the correct solution is not one unit but a staged system.
How a Venturi Scrubber Works
A venturi scrubber uses high gas velocity to atomize scrubbing liquid into fine droplets. Dust particles collide with these droplets and are captured. The dirty liquid is then separated from the gas in a downstream separator, cyclone, or demister section.
The basic sequence is:
- Gas enters the converging section.
- Gas velocity increases in the throat.
- Scrubbing liquid is injected into or before the throat.
- High turbulence creates fine droplets.
- Particles impact and attach to droplets.
- A separator removes liquid droplets from the cleaned gas.
The most important design variable is the pressure drop across the venturi throat. Higher pressure drop gives better particulate collection, especially for smaller particles, but it also increases fan power.
Typical operating ranges are:
- Gas velocity at throat: 50–120 m/s
- Pressure drop: 2–15 kPa
- Liquid-to-gas ratio: 0.5–3.0 L/m³ of gas, depending on dust loading and solubility
- Suitable particle size: usually >0.5 µm, with better efficiency as particle size increases
- Common material: PP, FRP, stainless steel, or special alloy depending on temperature and chemistry
A rough fan power estimate can be made from:
`text Fan power (kW) = Airflow (m³/s) × Pressure drop (Pa) ÷ Fan efficiency ÷ 1000 `
Example:
`text Airflow = 20,000 m³/h = 5.56 m³/s Venturi pressure drop = 6,000 Pa Fan efficiency = 0.65
Fan power ≈ 5.56 × 6,000 ÷ 0.65 ÷ 1000 Fan power ≈ 51 kW `
This is only the power for the pressure drop. Total fan selection must also include ducting, packed tower, demister, stack, dampers, and safety margin.
Comparing Venturi, Packed Bed, Cyclone, and Carbon Adsorber
A venturi scrubber should not be selected alone. It should be compared with other equipment according to pollutant type, dust loading, maintenance tolerance, and operating cost.
| Equipment | Best Use | Weak Point | Typical Pressure Drop | When to Use Before/After |
|---|---|---|---|---|
| Cyclone separator | Coarse dry dust, usually >5–10 µm | Poor for fine particles and mist | 0.5–2 kPa | Often before venturi if dust loading is high |
| Venturi scrubber | Fine dust, mist, soluble particles | Higher energy use, creates wastewater | 2–15 kPa | Before packed tower, carbon bed, or demister |
| Packed bed scrubber | Acid/alkali gas absorption | Packing can plug with solids | 0.8–2.5 kPa clean, higher if fouled | After venturi when gas pollutant removal is needed |
| Activated carbon adsorber | Low to medium VOC concentration | Sensitive to dust, mist, high humidity, high temperature | 0.8–2 kPa | After venturi and demister only if gas is dry enough |
This comparison is important for procurement. A low-cost single packed tower may look attractive, but if the inlet gas contains solid powder or sticky aerosol, it may require frequent shutdown for cleaning. A pre-scrubbing venturi can increase capital cost and fan power, but reduce plugging risk.
A typical combined arrangement is:
`text Process exhaust → Quench or dilution section if needed → Venturi scrubber → Droplet separator → Packed bed scrubber → Mist eliminator → Corrosion-resistant fan → Stack `
For VOC service, the arrangement may be:
`text Process exhaust → Venturi or wet pre-scrubber if particulate is present → Cooling and demisting → Dry filter or dehumidification if required → Activated carbon adsorber or other VOC treatment `
For activated carbon, the gas must normally be free of liquid droplets. Many carbon beds perform poorly if relative humidity is very high or if droplets carry dissolved solids into the bed. Therefore, after wet scrubbing, demisting and sometimes reheating or dilution may be required.
When Particulate Forces the Design Decision
Not every system needs a venturi scrubber. The key question is whether particulate will damage, plug, or reduce the performance of downstream equipment.
A venturi pre-scrubber should be considered when one or more of the following conditions apply:
- Dust loading is above 1–3 g/Nm³ and particle size is partly fine.
- Aerosol or mist is visible at the duct outlet.
- The gas contains sticky or hygroscopic particles.
- The downstream unit is packed media, carbon, catalyst, or heat exchanger.
- The process has batch peaks with short periods of high solids carryover.
- Existing packed tower pressure drop keeps increasing over time.
- Demister pads need frequent washing or replacement.
- The gas contains both particulate and soluble acid/alkali components.
For low dust loading, such as below 50–100 mg/Nm³, a packed scrubber with a good inlet distributor and washable mist eliminator may be enough. But this depends on particle type. A small amount of sticky resin mist can cause more trouble than a larger amount of non-sticky soluble salt.
Particle size also matters:
- >10 µm: cyclone or spray chamber may remove a large fraction.
- 2–10 µm: venturi scrubber becomes more useful.
- 0.5–2 µm: higher pressure drop venturi may be needed.
- <0.5 µm: efficiency depends strongly on pressure drop, particle properties, and droplet size; testing or conservative design is recommended.
The liquid chemistry must also be considered. If particles are soluble, water scrubbing may be effective. If acid or alkali gas is also present, chemical dosing may be needed. For example:
- HCl, HF, SO₂: usually alkaline scrubbing liquid
- NH₃: usually acidic scrubbing liquid
- Soluble salt dust: often water or controlled blowdown
- Organic sticky mist: may need special washing liquid and anti-fouling design
Blowdown rate is another practical issue. Captured particles do not disappear; they enter the scrubbing liquid. The sump must have enough volume, bleed-off, and access for sludge removal. For heavy solids, a cone-bottom tank or external settling tank may be required.
Key Design and Maintenance Points
A venturi scrubber is effective only when the mechanical and hydraulic design matches the process. The following points should be checked during engineering.
1. Gas flow range
Many process exhaust systems have variable flow. A fixed-throat venturi performs best in a narrower operating range. If airflow changes widely, an adjustable throat or multiple parallel lines may be considered. Very low flow reduces throat velocity and collection efficiency.
2. Pressure drop target
For general pre-scrubbing, 3–6 kPa is common. For fine particulate or mist, 6–10 kPa may be required. Above 10 kPa, collection can improve, but fan power and noise increase significantly. The optimum point depends on required outlet loading and operating cost.
3. Liquid distribution
Poor liquid injection causes dry zones and low collection efficiency. The nozzle or liquid entry should be accessible for inspection. For dirty liquid circulation, nozzle clogging must be considered. Large passages are preferred when solids are present.
4. Separator design
The venturi captures particles into droplets, but the droplets must then be removed. A badly sized separator can re-entrain liquid and send dirty mist downstream. Typical design checks include gas velocity, drain capacity, demister access, and wash nozzles.
5. Materials of construction
PP is widely used for corrosive acid and alkali gases at moderate temperature. As a general rule, PP equipment is commonly used below about 70–80°C, but the exact limit depends on chemical concentration, load, and structural design. Higher temperatures may need FRP, stainless steel, or other materials.
6. Maintenance access
A pre-scrubber handling solids must be designed for cleaning. Useful features include:
- Inspection doors at throat and separator
- Drain points at low sections
- Flush connections
- Removable spray nozzles
- Sump cleanout opening
- Differential pressure gauges across venturi and demister
- pH, conductivity, and liquid level monitoring where chemicals are used
A rising pressure drop across the venturi or separator often indicates fouling, blocked drains, excessive liquid flow, or demister plugging. A falling pressure drop may indicate reduced airflow, fan problem, or liquid injection failure.
Practical Next Step
Before selecting a venturi scrubber application, prepare the following data: airflow in normal and peak conditions, gas temperature, dust loading, particle size if available, pollutant gases, moisture level, chemical composition, and required outlet target. Also note whether the downstream equipment is a packed tower, carbon adsorber, fan, or stack only.
With these data, an engineer can compare a simple packed scrubber, cyclone plus scrubber, venturi plus packed tower, or wet pre-scrubber plus VOC treatment system. The correct choice should balance removal efficiency, pressure drop, wastewater handling, fouling risk, and maintenance access.


