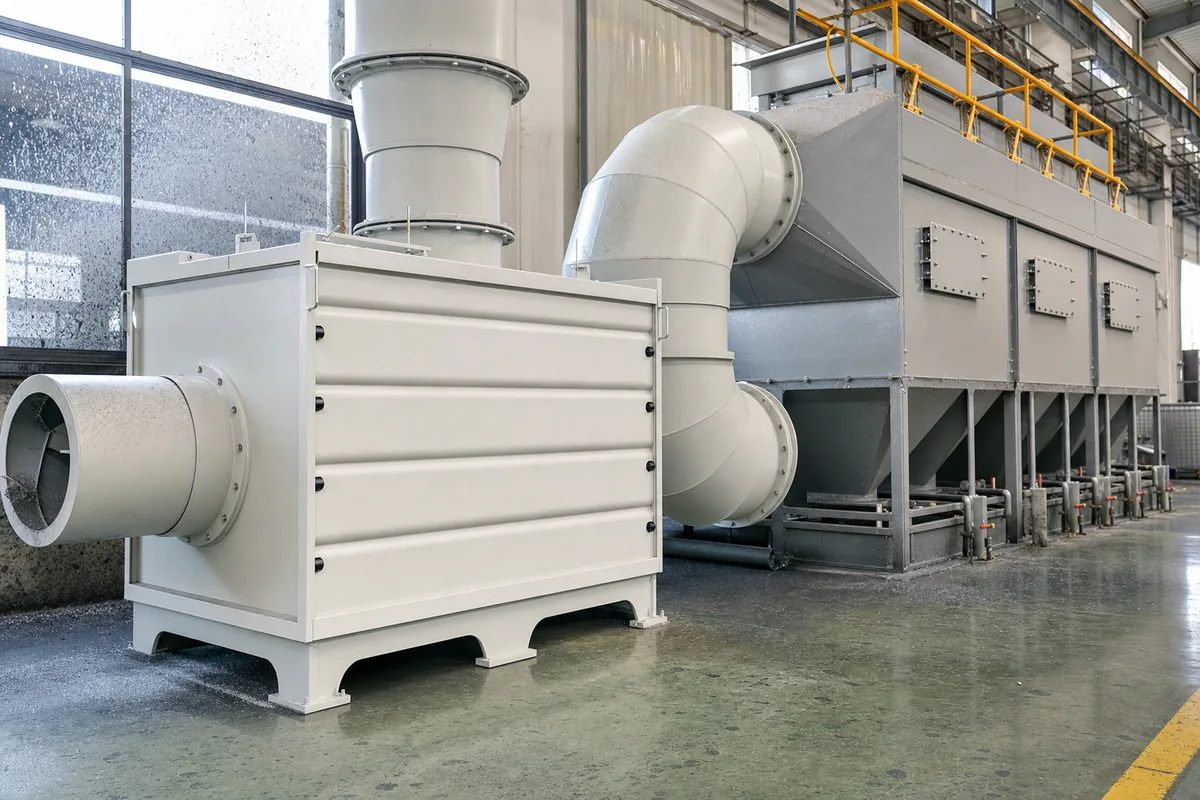
Why Carbon Beds Need Protection
Activated carbon is very good for many VOCs and odors, but it is a poor dust collector and a poor demister. If paint mist, powder dust, oil aerosol, acid mist, or water droplets enter the carbon bed, the pores are blocked before the adsorption capacity is used. The result is high pressure drop, short carbon life, uneven flow, and sometimes hot spots if solvent loading is high.
A correct pre filter before activated carbon is not one device in all cases. It is usually a small filtration train selected according to the contaminant:
- Paint overspray: sticky liquid/solid particles, often 5–50 µm, with resin content
- Dry dust: powder, sanding dust, pigment, fiber, or process solids, often 1–100 µm
- Water droplets: from scrubbers, washing towers, humid exhaust, or condensation
- Oil mist: compressor oil, machining oil, plasticizer aerosol, often sub-micron to several µm
- Acid or alkali mist: droplets from pickling, plating, etching, or chemical tanks
The target is simple: carbon should see mostly clean gas containing vapor-phase pollutants, not visible particles or droplets.
As a practical rule, install pre-filtration if any of these are true:
- You can see smoke, mist, paint fog, or dust in the duct.
- Wiping the inside of the duct leaves wet, oily, colored, or powdery residue.
- Exhaust relative humidity is near saturation or gas temperature is close to dew point.
- The upstream process includes spraying, grinding, coating, washing, cooling, or wet scrubbing.
- Existing carbon bed pressure drop rises quickly, for example doubling in weeks instead of months.
Identify the Contaminant Before Selecting the Filter
Before choosing the filter type, collect basic information. A short field check is often more useful than a long equipment list.
Measure or estimate:
- Air volume
Use actual operating flow in m³/h or CFM. Do not size filters only by fan nameplate. If possible, measure duct velocity and calculate: Q = A × V × 3600 where Q is m³/h, A is duct area in m², and V is velocity in m/s.
- Gas temperature and humidity
Activated carbon usually works better in dry gas. Many carbon beds should be kept below about 60–80% relative humidity when possible. Water competes for adsorption sites and may promote biological growth or corrosion in dirty systems.
- Particle or droplet type
Sticky paint mist needs depth media or multi-stage panels. Dry dust may need cartridge filtration. Large water droplets need a demister, not only a fabric filter.
- Solvent concentration
If VOC concentration is high, also check explosion and fire risk. Pre-filters can collect flammable paint solids or solvent-wet dust. This affects cleaning frequency, grounding, and safe operation.
- Available pressure
Every filter adds resistance. A common design allowance for a complete pre-filter section is 300–1000 Pa, depending on efficiency and dust loading. Confirm the fan can handle the final dirty-filter pressure, not only the clean condition.
Do not rely only on “filter grade” names. Different countries and suppliers use different classification systems. Ask for efficiency, recommended face velocity, initial pressure drop, and final pressure drop.
Common Pre-Filter Options and Where They Fit
The table below gives typical choices. Actual performance depends on media quality, housing sealing, air velocity, moisture, and contaminant loading.
| Contaminant before carbon | Typical pre-filter arrangement | Common face velocity | Initial pressure drop | Notes |
|---|---|---|---|---|
| Paint overspray from spray booth | Paint arrestor pad + bag or compact filter | 0.5–1.5 m/s at media face | 50–250 Pa per stage | Use depth media; change before paint dries hard and blocks airflow |
| Dry powder or sanding dust | Pleated panel + cartridge/bag filter | 0.8–2.0 m/s | 100–500 Pa | Add pulse cleaning for heavy dust; protect carbon from fine solids |
| Water droplets after wet scrubber | PP mesh pad demister or blade demister + drain | 1.5–3.0 m/s through vessel section | 100–400 Pa | Must include drainage; avoid re-entrainment at high velocity |
| Oil mist or fine aerosol | Coalescing filter or electrostatic/oil mist separator + final filter | Depends on type | 200–1000 Pa | Oil quickly blinds carbon; use washable or drainable stages |
| Acid/alkali mist | PP/PVC demister + corrosion-resistant housing | 1.5–3.0 m/s | 100–500 Pa | Materials must match chemical; add wash access if crystallization occurs |
| General light dust | G4/M5 type pre-filter + F7/F8 type fine filter, or equivalent | 1.0–2.5 m/s | 100–450 Pa | Suitable for low loading; not for sticky overspray |
For many VOC systems, a two-stage layout is effective:
- Coarse pre-filter to catch large particles or droplets.
- Fine filter or demister to protect carbon from carryover.
For severe paint mist, three stages may be required:
- Cardboard labyrinth or glass fiber paint arrestor
- Synthetic bag filter
- Fine panel or compact filter before carbon
For exhaust after a wet scrubber, do not install only a dry fabric filter immediately downstream if water carryover is present. A demister with drainage should be first. Fabric filters become wet, grow biological slime, or collapse if not designed for wet service.
Sizing Rules That Prevent Early Failure
A pre-filter before activated carbon fails early mainly because of high velocity, poor sealing, no drain, or no maintenance access.
1. Keep velocity low enough
High face velocity pushes particles through the media and increases pressure drop. It can also pull captured droplets off a demister.
Useful starting points:
- Paint arrestor media: 0.5–1.5 m/s
- Bag filters for general dust: 1.0–2.0 m/s
- Compact fine filters: 1.5–2.5 m/s, depending on supplier data
- Mesh pad demister in a vessel: 1.5–3.0 m/s
- Duct velocity before filter box: commonly 8–15 m/s, then expanded before filter
Filter area can be estimated by:
Filter face area = Airflow / Face velocity
For example, for 10,000 m³/h and a desired media face velocity of 1.2 m/s:
10,000 / 3600 / 1.2 = 2.31 m²
So the filter bank should provide at least about 2.3 m² of open face area, before considering frame blockage and layout.
2. Design for dirty pressure drop
Do not size the fan using only clean filter resistance. A typical replacement point may be:
- Coarse panel filter: final pressure drop 150–250 Pa
- Bag filter: final pressure drop 300–600 Pa
- Fine compact filter: final pressure drop 400–800 Pa
- Demister: clean 100–300 Pa, but higher if fouled or flooded
The control panel should include a differential pressure gauge or transmitter across the filter section. A simple U-tube manometer is acceptable for many systems if operators read it.
3. Seal the filter bank
If air bypasses the filter, the carbon bed still becomes dirty. Provide:
- Gasketed filter frames
- Clamping mechanism, not loose sliding only
- Access doors with rubber seals
- No open gaps around filter edges
- Drain traps for wet sections
Small bypass gaps can defeat expensive filters. A 5 mm gap along a frame may carry significant unfiltered air because it has lower resistance than the media.
4. Control condensation
If warm humid gas cools in the duct or filter box, water will condense. Carbon will then adsorb less VOC and may develop high pressure drop.
Check approximate dew point conditions. If gas temperature may fall below dew point, consider:
- Insulating ductwork
- Locating carbon closer to the process
- Reheating gas slightly after a scrubber
- Adding a knockout section and drain before dry filters
- Using a demister before any fine dry media
For many carbon adsorption systems, gas temperature around 20–40°C and relative humidity below 60–70% is easier to handle. Higher humidity is possible, but carbon life and adsorption capacity should be checked for the specific VOC.
Installation and Maintenance Details
Good pre-filtration is a maintenance system, not only a filter purchase. The filter housing should be designed so operators can replace media safely and quickly.
Recommended details:
- Install straight duct before and after the filter box when possible. A rule of thumb is 3–5 duct diameters upstream if space allows.
- Provide access doors on the clean side and dirty side for inspection.
- Add internal supports so wet or loaded filters do not sag.
- Use corrosion-resistant materials. For acidic or alkaline exhaust, PP, FRP, PVC, or coated steel may be needed depending on temperature and chemical concentration.
- Install a drain at the lowest point of demister and wet filter sections.
- Avoid placing activated carbon directly after a wet scrubber without a demister.
- Keep spare filter sets on site, especially for paint lines and batch operations.
- Label airflow direction on the housing and filter frames.
Maintenance intervals depend strongly on the process. General guidelines:
- Paint arrestor: inspect daily to weekly; replace when loaded or pressure drop reaches the set point.
- Dust pre-filter: inspect weekly at first, then set interval based on differential pressure trend.
- Demister: inspect monthly to quarterly; wash if deposits, salts, or sludge are visible.
- Carbon bed: record pressure drop and outlet VOC/odor condition; sudden pressure rise often indicates upstream filtration failure.
A useful practice is to record four values in a log sheet:
- Date
- Airflow or fan frequency
- Pressure drop across pre-filter
- Pressure drop across carbon bed
If the carbon bed pressure drop rises while pre-filter pressure stays normal, check for bypass, moisture carryover, or internal carbon settling. If pre-filter pressure rises quickly, the selected media may be too fine for the first stage or the filter area may be too small.
Practical Next Step
Before ordering or modifying a carbon adsorber, make a simple contaminant map: list each upstream source, whether it creates dust, paint mist, oil, water droplets, or chemical mist, and the airflow from each source. Then select a pre filter before activated carbon based on the worst contaminant, not only the VOC name. If you can provide airflow, temperature, humidity, contaminant type, and photos of the duct or existing filters, a supplier can recommend a suitable filter train and pressure-drop allowance.


