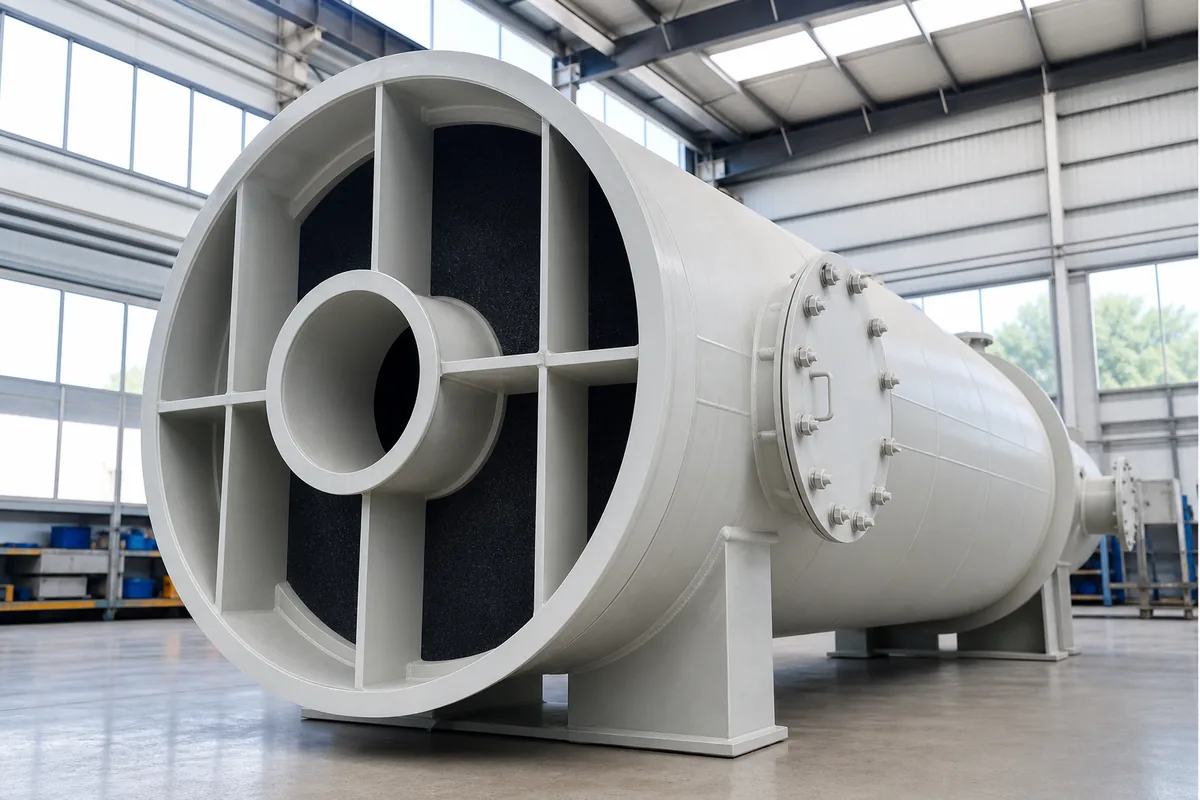
Why Bed Velocity Controls Adsorber Performance
In an activated carbon adsorber, many engineers first ask for carbon weight or tank size. Those are important, but the operating number that often decides success or failure is carbon bed face velocity.
Face velocity is the superficial gas velocity through the carbon bed:
`text carbon bed face velocity = gas flow rate / bed cross-sectional area `
In SI units:
`text v = Q / A `
Where:
v= face velocity, m/sQ= actual gas flow rate, m³/sA= carbon bed face area, m²
For example, if an adsorber handles 10,000 m³/h:
`text Q = 10,000 / 3,600 = 2.78 m³/s `
If the bed face area is 5.6 m²:
`text v = 2.78 / 5.6 = 0.50 m/s `
This number affects:
- Contact time between VOC molecules and carbon
- Pressure drop through the bed
- Risk of carbon dust movement and channeling
- Carbon utilization before breakthrough
- Required fan static pressure
- Adsorber vessel size and layout
For most fixed-bed VOC adsorption systems, a practical design range is usually 0.2 to 0.6 m/s. Many industrial systems operate around 0.3 to 0.5 m/s. The correct value depends on VOC type, inlet concentration, humidity, temperature, removal target, carbon type and whether the unit is single-use or regeneration type.
If the velocity is too high, the gas passes through the bed before the VOC has enough time to diffuse into the carbon pores. The result is early breakthrough, even if the adsorber contains a large amount of carbon.
How to Calculate Face Velocity Correctly
Always calculate face velocity using actual gas flow, not normal flow, unless the gas is already converted to operating temperature and pressure.
If your process flow is given as Nm³/h, convert it to actual m³/h:
`text Qactual = Qnormal × (Tactual / Tnormal) × (Pnormal / Pactual) `
Using absolute temperature in Kelvin:
`text T(K) = °C + 273.15 `
Example:
- Normal flow: 8,000 Nm³/h
- Normal condition: 0°C, 1 atm
- Actual gas temperature: 45°C
- Actual pressure: approximately 1 atm
`text Qactual = 8,000 × (318.15 / 273.15) Qactual = 9,318 m³/h `
If the adsorber bed area is 4.5 m²:
`text v = 9,318 / 3,600 / 4.5 v = 0.58 m/s `
That is already near the upper end for many VOC carbon beds.
For rectangular horizontal beds:
`text A = width × length `
For vertical cylindrical beds with upward or downward gas flow:
`text A = π × D² / 4 `
Where D is the internal diameter.
Be careful with multi-bed designs. If two beds operate in parallel, divide the total gas flow by two before calculating each bed velocity. If two beds are in series, each bed sees the full gas flow, so the face velocity is the same through both beds.
A useful quick check:
`text Required bed area = actual gas flow / target face velocity `
For 15,000 m³/h actual flow and a target velocity of 0.45 m/s:
`text A = (15,000 / 3,600) / 0.45 A = 9.26 m² `
So the adsorber needs about 9.3 m² of active bed face area.
Typical Velocity Ranges and When to Use Them
The correct carbon bed face velocity is not one fixed value. It must match the duty. The table below gives practical starting points for engineering discussion.
| Application condition | Typical face velocity | Notes |
|---|---|---|
| Low concentration VOC, easy-to-adsorb solvents | 0.4–0.6 m/s | Suitable when removal target is moderate and breakthrough time is not critical |
| Mixed VOCs with unknown composition | 0.3–0.45 m/s | Safer range when adsorption behavior is uncertain |
| High removal efficiency requirement | 0.2–0.35 m/s | Longer contact time improves carbon utilization |
| High humidity gas | 0.25–0.4 m/s | Water vapor competes for adsorption sites; slower velocity helps but pretreatment may be needed |
| Odor control with trace contaminants | 0.2–0.5 m/s | Depends strongly on odor threshold and compound type |
| Regenerative carbon system | 0.2–0.4 m/s | Often designed with lower velocity for stable cycle performance |
| Emergency or intermittent polishing duty | 0.4–0.6 m/s | Acceptable if loading is low and breakthrough monitoring is used |
Velocity should be considered together with empty bed contact time, often called EBCT:
`text EBCT = carbon bed depth / face velocity `
Where:
EBCT= seconds- Bed depth = m
- Face velocity = m/s
Example:
- Bed depth: 0.8 m
- Face velocity: 0.4 m/s
`text EBCT = 0.8 / 0.4 = 2.0 seconds `
For many VOC adsorption duties, EBCT is commonly in the range of 1 to 3 seconds. Difficult applications may require more. Very easy polishing duties may work with less, but this should be confirmed by adsorption data or operating experience.
A deeper bed is not always a solution if face velocity is too high. Deep beds increase contact time, but they also increase pressure drop and carbon inventory. If gas distribution is poor, a deeper bed may still develop channeling.
What Happens When Velocity Is Too High or Too Low
High face velocity usually causes more problems than low velocity.
When velocity is too high:
- VOC breakthrough happens earlier than calculated
- Pressure drop increases
- Fan power increases
- Carbon fines may move or collect at screens
- Gas distribution becomes less uniform
- Effective carbon capacity decreases
- Local hot spots may become more likely in high-loading applications
Pressure drop is especially important. Carbon bed pressure drop depends on carbon particle size, bed depth, gas temperature, dust loading and moisture. As a rough engineering range, clean activated carbon beds may show about 800 to 2,500 Pa per meter of bed depth at typical industrial velocities. This is only a starting estimate. Smaller carbon particles and higher velocity can increase pressure drop sharply.
Fan power can be estimated as:
`text Power = Q × ΔP / η `
Where:
Power= WQ= m³/sΔP= Paη= fan and motor efficiency as decimal
Example:
- Gas flow: 12,000 m³/h = 3.33 m³/s
- Total system pressure: 2,800 Pa
- Efficiency: 0.60
`text Power = 3.33 × 2,800 / 0.60 Power = 15,540 W `
So a motor around this range, with proper design margin, would be considered. Final motor selection must include duct loss, dampers, scrubber loss if used, safety margin and local electrical requirements.
Very low face velocity is not always ideal either. It makes the adsorber larger and may increase equipment footprint. In some horizontal beds, very low velocity combined with poor inlet design can also allow uneven gas distribution. Low velocity is good for adsorption, but the vessel still needs proper plenum design, perforated plates or distribution screens, and enough straight inlet distance.
A practical warning: do not size an adsorber only by carbon mass. Two units may both contain 1,000 kg of carbon, but if one has a small bed area and high velocity, it may perform much worse.
Design Checks Before Ordering a Carbon Adsorber
Before selecting a carbon adsorber, check these items with your supplier or internal process team.
1. Actual gas flow
Confirm maximum, normal and minimum flow. Include temperature, pressure and moisture. If the exhaust fan is controlled by VFD, define the design flow at full production.
2. VOC concentration and composition
Carbon capacity depends strongly on the compound. Toluene, xylene and many heavier solvents adsorb better than methanol, acetone or very light organics. Mixtures are more complex because strong adsorbing compounds can displace weak ones.
3. Temperature
Many activated carbon systems work best below about 40°C. Higher temperature reduces adsorption capacity. Some applications can operate above this, but the breakthrough time may be shorter. Cooling or upstream wet scrubbing may be required depending on the gas.
4. Humidity
High relative humidity reduces capacity, especially for water-soluble or weakly adsorbed VOCs. If relative humidity is above 70–80%, discuss pretreatment, demisting, reheating or a larger bed.
5. Dust and mist
Carbon beds are not good dust filters. Particulate, oil mist, resin mist or acid mist can block pores and increase pressure drop. Use a pre-filter, demister or wet scrubber where needed.
6. Bed depth
Common fixed beds often use 0.5 to 1.2 m carbon depth. Shallow beds reduce contact time. Very deep beds increase pressure drop and carbon replacement labor. The correct depth depends on EBCT and carbon change-out interval.
7. Gas distribution
The inlet plenum should avoid jetting directly into the carbon. Poor distribution creates high local velocity. Even if the calculated average face velocity is 0.4 m/s, part of the bed may see 0.8 m/s if the inlet is badly designed.
8. Monitoring
For important VOC duties, include sampling ports before and after the adsorber. A differential pressure gauge or transmitter across the bed is also recommended. Rising pressure drop may indicate dust loading, moisture, carbon settling or blocked screens.
Practical Next Step
To check whether your carbon adsorber is correctly sized, prepare four numbers first:
- Maximum actual exhaust flow, m³/h
- Bed face area, m²
- Carbon bed depth, m
- Gas temperature and main VOC components
Then calculate:
`text face velocity = actual flow / 3,600 / bed area EBCT = bed depth / face velocity `
If the face velocity is above 0.6 m/s or EBCT is below about 1 second, review the design before purchasing or operating at full load. If the gas is hot, humid, dusty or contains difficult VOCs, use a more conservative velocity range and discuss pretreatment.


